Brands moving production to Europe
Re-industrialize an existing frame for a new factory.
See the steps →Independent product engineering and industrialization for bicycle and e-bike brands. Led by Anton Nastev, who co-founded and ran an aluminium frame factory.

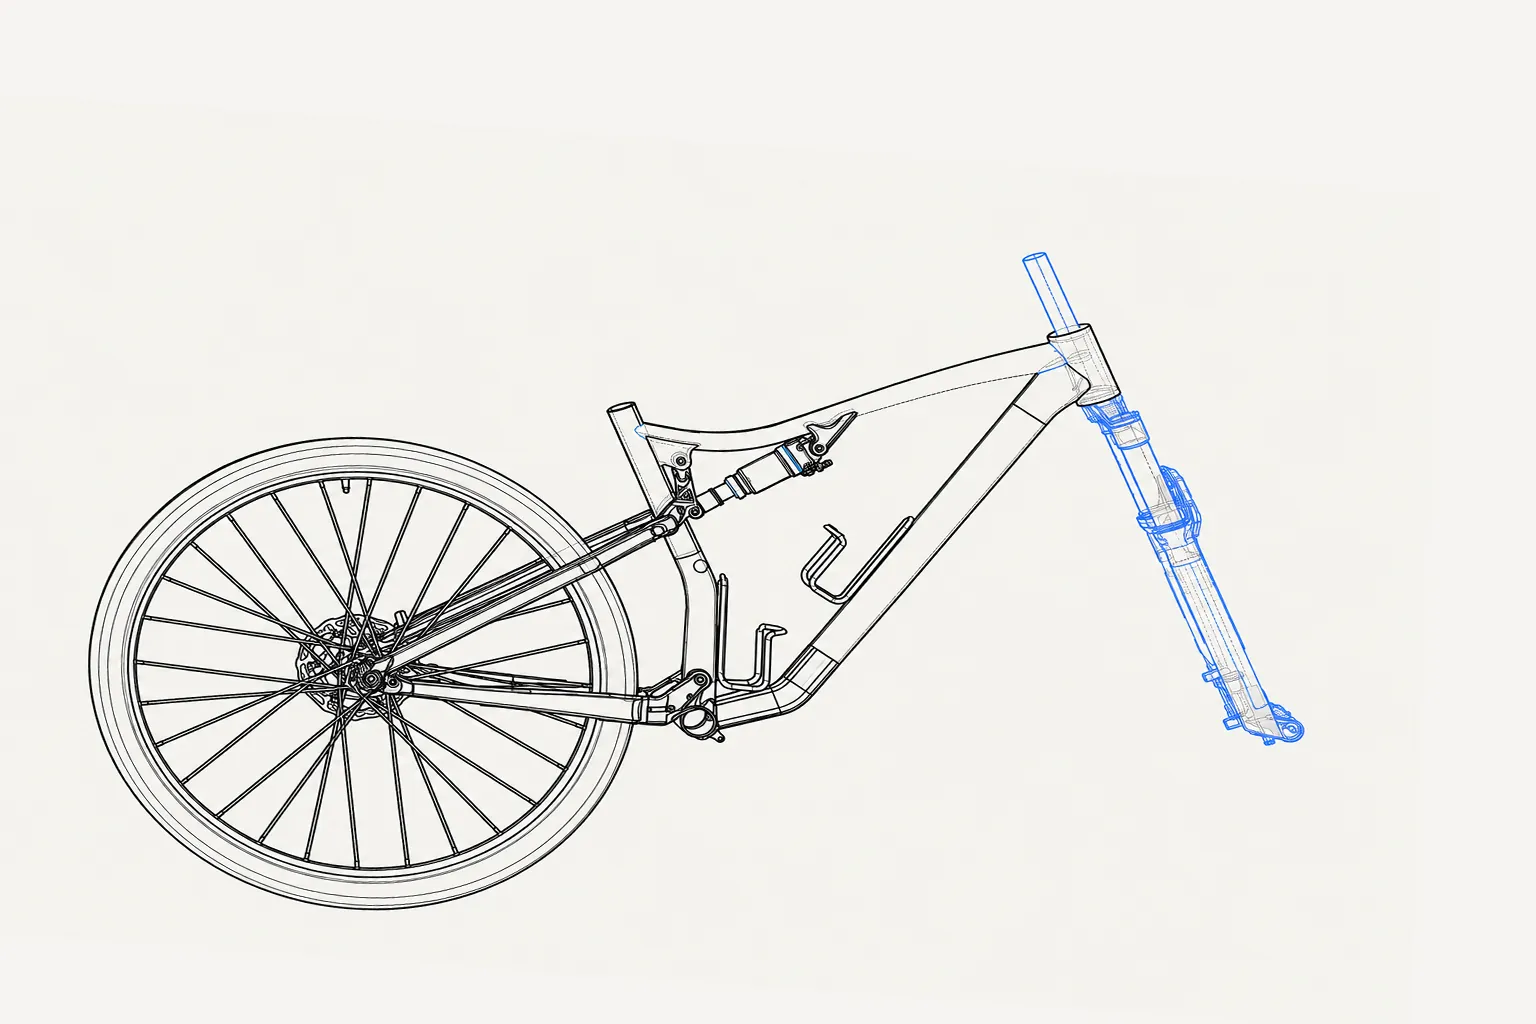
A prototype that rides well still has to become a frame built in thousands. That is where programmes lose time.
of a product’s cost is committed at the design stage. Changes are cheapest on the drawing.Source: Boothroyd Dewhurst, DFMA
Every tube, link and pivot of a full-suspension frame, modelled and checked before anything is cut.

The steps stay the same. The loops back between them go.
Test regime, cost and volume fixed before geometry.
Suppliers review the design before they quote.
Every sample round answers a defined question.
The longest-lead dies are identified at G3, before design freeze.
The pilot is measured against a written standard.
Each programme enters the process at a different step.
Re-industrialize an existing frame for a new factory.
See the steps →Plan the lab test before the first sample is built.
See the steps →From first weld to stable serial yield.
See the steps →From sketch to series, with one accountable lead.
See the steps →Engineering due diligence on a frame operation.
See the steps →Nine steps and seven decision gates. Most programmes join part-way through.
A market idea turned into a brief engineers can build against.
The test regime is known before any geometry exists.
ANVILDrafts the specification and runs the review.
YouOwn the market brief and sign off G1.
Geometry and manufacturing route, decided before metal is cut.
The manufacturing route is chosen once, before the first quote arrives.
ANVILLeads the engineering.
You / studioOwn the industrial design and sign off G2.
The design adapted to the factory that will build it.
The redesign that usually follows the first quote happens on paper.
ANVILLeads the DFM, the RFQ and the tooling plan.
SuppliersReview and quote.
YouApprove the release.
Lab-tested against a written plan, to EN ISO 4210 or EN 15194.
The tooling budget is committed only once the design holds.
ANVILWrites the plan and analyses the results.
Prototype supplierBuilds the samples.
Accredited labRuns the tests and issues the reports.
YouSign off the freeze.
Process, tooling and suppliers, qualified before the pilot.
Control plan and Q-gates, written alongside the process.
Tooling and supplier problems surface at tryout and audit, before the pilot batch.
ANVILDefines the process and audits suppliers.
FactoryBuilds tooling, runs tryouts.
YouApprove investments.
The pilot is measured against a standard written in advance.
ANVILWrites the plan, trains the team.
FactoryRuns it.
YouApprove it.
The process proven on production tooling, at rate.
Problems are found in a pilot batch, before the first serial shipment.
FactoryRuns the pilot.
ANVILWitnesses, analyses and prepares the release.
LabRuns the production-validation tests.
YouRelease production.
From the first serial frame to stable full-rate output.
Containment exit criteria are written in advance, so the ramp-up has a defined end.
FactoryProduces.
ANVILMonitors and hands over.
YouAccept the handover.
Data from your own line drives cost and quality.
The next model year starts from a capable process with known data.
ANVILAnalyses and proposes.
Your teamImplements.
YouSet priorities.
Start at your step
Start a projectOne part followed from Anton’s own work: the CAD model, the machined rocker, the frame prototype and the bike it went into.
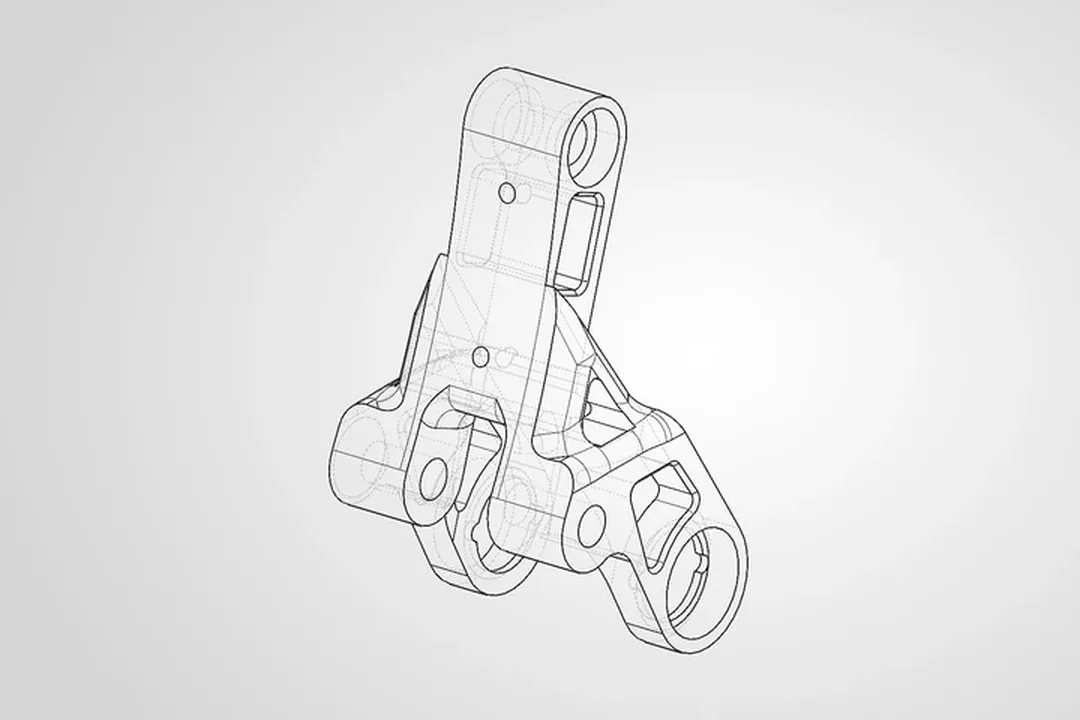
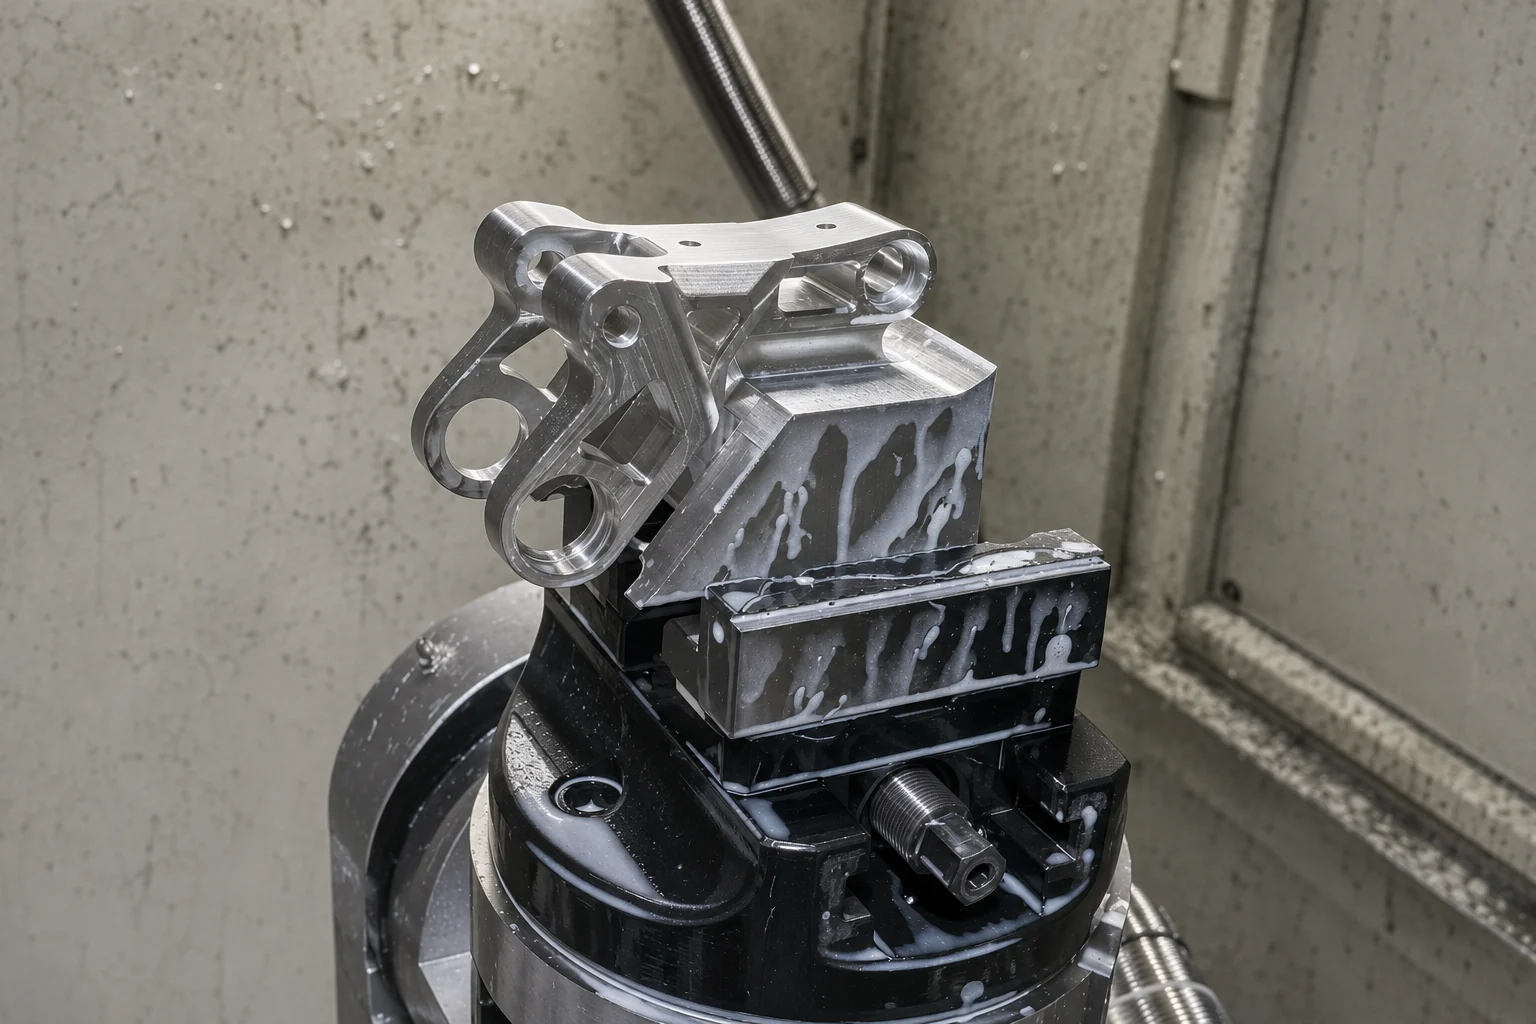
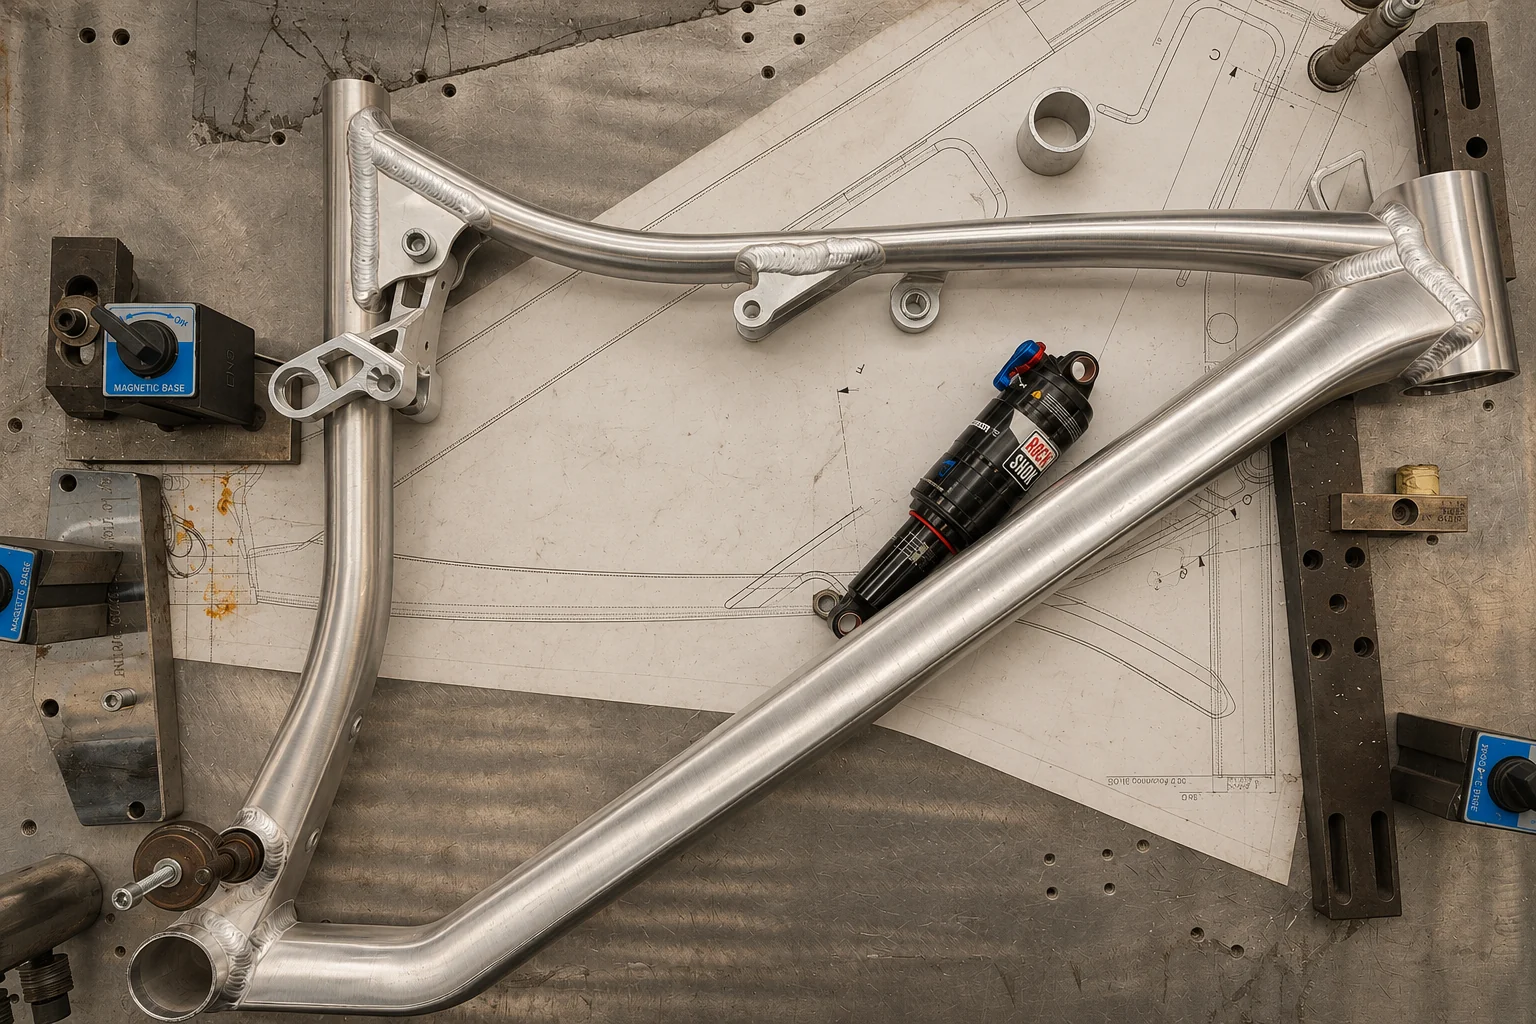
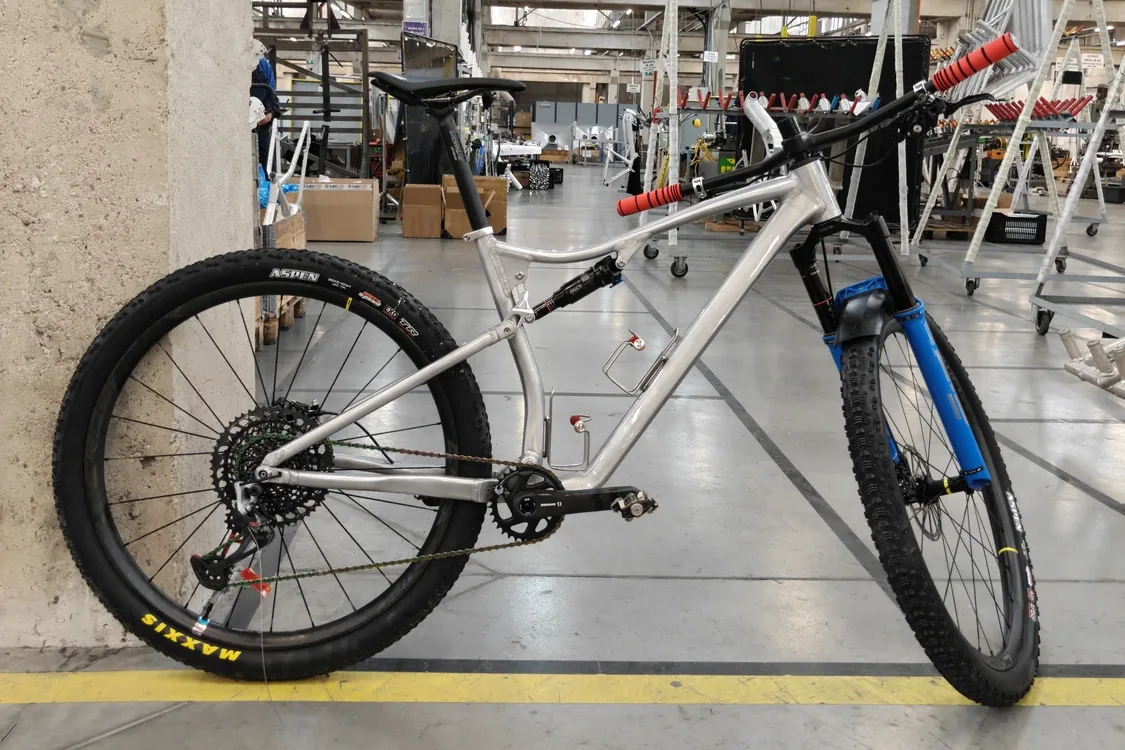

Twelve disciplines, built hands-on in frame development and production.
Validation is planned to EN ISO 4210, EN 15194, EN 17404 or EN 17860, as the product requires. Accredited independent labs run the tests.
Four ways in, from a short diagnostic to a long-term role.
Where the programme stands and what to fix first. A written report you keep.
Ask for a diagnostic →One accountable engineering lead for an agreed range of steps.
Discuss a programme →Senior industrialization lead, a fixed number of days per month.
Discuss a fractional role →Audits, tryouts, pilot runs and welder training, on site.
Request support →Mechanical engineer · MSc Automotive Technology, TU Eindhoven
More than fifteen years in the bicycle industry. He co-founded an aluminium frame factory near Sofia and took it from an empty hall to serial production: hydroforming, welding, heat treatment, machining and quality gates.
Career profile on LinkedIn